A Green Torque Light Is Not a Traceable Rail Maintenance Record
A torque-tool pass is only one part of railway maintenance evidence. Before a safety-related bolted joint is released, the maintenance record must connect the correct vehicle, assembly, joint location, work order, approved procedure, tool, operator and inspection decision. If a result is missing, incomplete or associated with another vehicle, the discrepancy must be resolved through the authorized maintenance process before release.
The green torque light in this article title is a metaphor for a tool’s pass indication. It is not a claim that a green indicator was reported in the railway incident discussed below.
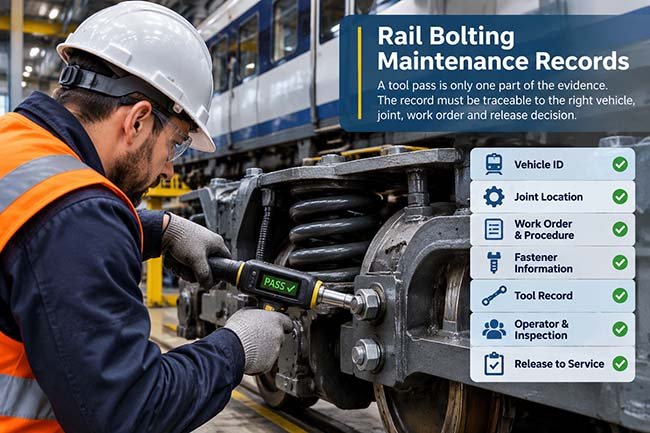
Table of Contents
- Why a Torque Tool Pass Is Not Enough
- A Railway Maintenance Case: What Went Wrong?
- What Makes a Rail Bolting Record Traceable?
- Joint-to-Tool Record Identity Matrix
- Shift Handover: Where Maintenance Records Can Break Down
- Maintenance Release Evidence Checklist
- What Railway Maintenance Standards Say About Traceability
- Frequently Asked Questions
1. Why a Torque Tool Pass Is Not Enough
Modern maintenance workshops may use electronic torque tools to capture tightening results. These tools can improve measurement recording and help maintenance teams review completed work.
However, a tool result and a complete maintenance record are not the same thing.
A tool may record a successful tightening event, but the result still needs to be associated with the correct vehicle and joint.
For example, consider a hypothetical maintenance situation:
An electronic torque tool records a successful result. However, the maintenance database associates that result with Vehicle 1122, while the physical work was performed on Vehicle 1121.
The tool event may be genuine, but its identity association is incorrect.
Can the maintenance team use that record to release the vehicle?
Not without resolving the discrepancy through the approved quality and maintenance process.
The problem is not necessarily the measured value. It is whether the available evidence proves that the required work was completed on the correct asset.
What a Tool Result Can and Cannot Establish
| Evidence | What It Can Establish | What It Does Not Establish by Itself |
|---|---|---|
| Tool pass indication | A result met the tool’s configured acceptance condition | Correct vehicle or joint identity |
| Electronic tightening record | Recorded measurement data from a tightening event | Completion of every required fastening operation |
| Tool identification | Which tool generated the record | Whether the correct procedure and program were selected |
| Operator identification | Who performed the recorded operation | Whether the full work package was completed |
| Supervisor sign-off | A documented review or approval | Missing underlying measurements or unidentified work |
| Maintenance release | Authorized completion status under the applicable procedure | Unrecorded or unresolved work outside the release scope |
A torque value should always be evaluated against the applicable vehicle-specific procedure. This article does not provide universal torque settings, tightening sequences or acceptance limits for railway equipment.
2. A Railway Maintenance Case: What Went Wrong?
The Ottawa Light Rail Transit derailment in September 2021 provides a documented example of why maintenance records and work handovers matter.
The Ottawa Light Rail Transit Public Inquiry Final Report, November 2022 examined the circumstances surrounding the incident.
The investigation concerned LRV 1121, which was returned to passenger service after bogie maintenance and refurbishment work.
The inquiry established that bolts in the bogie assembly had not been properly tightened following disassembly. The motor gearbox subsequently became detached, resulting in a derailment.
The Commission also identified several maintenance quality problems:
- Inadequate checklists for safety-critical assembly and repair work.
- Insufficient maintenance records.
- Inadequate supervisory and quality-control review.
- Weaknesses in communicating incomplete work between shifts.
The report specifically emphasized the importance of qualified supervisory or quality-control personnel reviewing and approving completed work, particularly when maintenance begins on one shift and continues on another.
This was not simply a problem with an individual fastening operation. It demonstrated how incomplete work, insufficient documentation and weak handover arrangements can combine to undermine maintenance control.
The event is a specific Ottawa LRT case, not evidence that all railway maintenance workshops have the same problems.
For maintenance planners and depot QA teams, the key lesson is that a completed tool operation must be connected to a complete and verifiable work record.
3. What Makes a Rail Bolting Record Traceable?
A useful maintenance record should allow an independent reviewer to answer five questions:
- Which vehicle was maintained?
- Which exact connection was worked on?
- Which approved procedure and fastener specification applied?
- Who performed and verified the work?
- What evidence supports the final release decision?
These questions can be organized into a traceability chain.
The Maintenance Traceability Chain
Vehicle Identity → Work Order → Joint Identification → Procedure Revision → Fastener Identification → Tool Record → Operator → Inspection → Release
Each link should be connected to the next.
For example, a tightening result should not exist as an isolated data row without a clear reference to the work order and connection location.
Similarly, a completed work order should not be treated as proof that every required fastening event has been recorded and accepted.
Seven Essential Record Categories
| Record Category | Information to Capture | Why It Matters |
|---|---|---|
| Asset identity | Vehicle number, fleet number and applicable configuration | Identifies the correct vehicle |
| Joint identity | Bogie, axle, wheel position or specific connection reference | Identifies the actual work location |
| Work specification | Work order, job card, procedure number and revision | Establishes the approved maintenance requirements |
| Fastener identity | Part reference, specification and batch or lot where required | Connects the installed components to procurement records |
| Tool information | Tool ID, calibration or verification status and applicable program reference | Identifies the measurement equipment |
| Execution record | Recorded result, operator, date, time and completion status | Documents the work performed |
| Quality release | Inspection, exception disposition and authorized approval | Supports the release decision |
This is an editorial traceability framework for maintenance planning. The actual mandatory fields should follow the operator’s approved quality system, OEM requirements and applicable regulations.
4. Joint-to-Tool Record Identity Matrix
The most practical way to prevent record mismatches is to make the relationship between the physical connection and the digital tool record explicit.
The following matrix can be used when designing a maintenance database, reviewing workshop records or auditing a completed work package.
| Identification Level | Required Reference | Verification Question |
|---|---|---|
| Vehicle | Fleet or vehicle number | Does the record belong to the correct vehicle? |
| Assembly | Bogie or equipment identification | Does the record identify the correct assembly? |
| Connection | Axle, wheel position or joint reference | Is the actual fastening location identifiable? |
| Work order | Maintenance order or job card | Is the work authorized and properly defined? |
| Procedure | Document number and revision | Was the applicable procedure identified? |
| Fastener | Part number and batch reference where applicable | Can the supplied hardware be traced to the work package? |
| Tool | Tool serial number and calibration status | Is the equipment identifiable and suitable for the recorded measurement? |
| Tightening event | Unique event or record reference | Can the tool result be linked to the correct joint? |
| Operator | Authorized personnel identification | Who performed the work? |
| Quality review | Reviewer and approval reference | Who verified completion and resolved exceptions? |
Example: How a Record Mismatch Should Be Handled
Suppose a maintenance system contains a valid tool record, but the vehicle number does not match the physical work order.
The record should be classified as Identity Mismatch – Hold for Review.
The responsible team should:
- Preserve the original tool record.
- Identify the physical vehicle and connection.
- Compare the maintenance order, work sequence and tool event.
- Investigate the source of the mismatch.
- Obtain the required authorized correction or disposition.
- Preserve the original record and the audit trail of any correction.
- Confirm the release decision through the approved process.
Do not simply overwrite the vehicle number or manually move a successful result into another work order without documented reconciliation.
An audit trail is important because a corrected database entry should not conceal what was originally recorded.
5. Shift Handover: Where Maintenance Records Can Break Down
Rail maintenance often involves multiple technicians, supervisors and shifts.
A maintenance task may start on one shift, continue on another and receive final inspection from a separate quality team.
This creates a potential gap between the physical status of the assembly and the status recorded in the maintenance system.
A work order marked as completed may not provide sufficient evidence if some fastening operations remain outstanding.
Suggested Shift Handover Exception Log
| Handover Field | Information to Record |
|---|---|
| Vehicle identification | Vehicle and fleet number |
| Assembly location | Bogie, axle or relevant connection |
| Work order | Maintenance order reference |
| Procedure | Applicable procedure and revision |
| Completed work | Specific operations already completed |
| Outstanding work | Unfinished fastening or inspection activities |
| Tool records | Existing record references and missing results |
| Fastener status | Components installed, outstanding or awaiting verification |
| Exceptions | Failed results, missing data or identification discrepancies |
| Vehicle status | Maintenance hold or other authorized status |
| Outgoing shift | Responsible person and handover time |
| Incoming shift | Receiving person and acknowledgement |
| Supervisor | Responsible reviewer or escalation contact |
This log should make outstanding work visible rather than relying on verbal communication alone.
Three Handover Conditions
Condition A: Work Completed and Recorded
The required operations have been completed, the relevant records are available and the applicable review has been performed.
Condition B: Work Partially Completed
The next shift receives a clear list of unfinished operations and the vehicle remains under the required maintenance control.
Condition C: Records Cannot Be Reconciled
The vehicle, joint or tool record contains conflicting information. The discrepancy is escalated, and the release decision remains open until it is resolved.
The handover form is an editorial tool, not a substitute for the operator’s formal work authorization or vehicle movement controls.
6. Maintenance Release Evidence Checklist
Before closing a safety-related bolting work package, the maintenance and quality teams should confirm that the necessary evidence is available.
| Release Check | Evidence to Review | Status |
|---|---|---|
| Correct vehicle | Vehicle identity and configuration | Open / Accepted |
| Correct work location | Joint or assembly reference | Open / Accepted |
| Correct procedure | Approved maintenance document and revision | Open / Accepted |
| Fastener identity | Applicable part and material records | Open / Accepted |
| Tool identity | Tool ID and calibration or verification record | Open / Accepted |
| Tightening results | Required tool records and acceptance results | Open / Accepted |
| Work completeness | All required operations accounted for | Open / Accepted |
| Exceptions | Missing results and deviations resolved | Open / Accepted |
| Handover | Outstanding work and shift records reconciled | Open / Accepted |
| Final inspection | Required verification completed | Open / Accepted |
| Authorization | Required supervisor or quality approval | Open / Accepted |
| Release | Authorized release-to-service documentation | Open / Accepted |
When Should a Work Package Be Held?
The following conditions should trigger review under the applicable maintenance procedure:
- The vehicle or connection identity cannot be confirmed.
- Required tool records are missing.
- A tool result cannot be linked to the relevant work order.
- The maintenance procedure revision is uncertain.
- An operation remains outstanding after shift handover.
- A failed result or deviation has no documented disposition.
- Required inspection or approval is incomplete.
A green tool indication must not override an unresolved maintenance record.
7. What Railway Maintenance Standards Say About Traceability
Railway maintenance documentation is not merely an administrative exercise. It is part of the wider maintenance and safety-management framework.
7.1 European Union: Regulation (EU) 2019/779
The European Commission’s Implementing Regulation (EU) 2019/779 establishes requirements for entities in charge of maintenance of railway vehicles.
The regulation distinguishes two important concepts:
- Release to service: A justified and recorded assurance that maintenance has been delivered according to the maintenance orders.
- Return to operation: A notice based on release-to-service documentation confirming that the required maintenance has been completed and the vehicle is safe to use, subject to any applicable restrictions.
Annex II also addresses:
- Accuracy and completeness of vehicle identification information.
- Maintenance documentation and records.
- Personnel qualifications and supervision.
- Identification of maintenance tools and equipment.
- Calibration and verification of measuring equipment.
- Traceability of safety-related documentation.
- Maintenance work, materials and tools used.
- Final testing and release decisions.
These provisions provide a useful regulatory reference for understanding why vehicle identity, maintenance records, tool information and release documentation must be connected.
Scope limitation: This is an EU regulatory framework. Its specific applicability and certification obligations depend on the organization, vehicle and applicable legal requirements. It should not be presented as a universal global railway maintenance standard.
7.2 Railway Quality Management: ISO 22163:2023
ISO 22163:2023 establishes a railway quality management system based on ISO 9001:2015, with additional requirements for the railway sector.
Its published scope covers organizations across the railway industrial supply chain and emphasizes defect prevention, continual improvement and product quality, including safety aspects.
It provides broader quality-management context for organizations involved in railway products and services.
However, the public scope alone does not prescribe a universal torque-record format or prove that a specific maintenance process is compliant.
The actual record structure and acceptance criteria must follow the applicable maintenance procedures and customer requirements.
8. Frequently Asked Questions
Q1. Does an electronic torque tool record prove that a railway joint is correctly tightened?
Not by itself. It provides evidence of a recorded tool event, but the result must also be associated with the correct vehicle, joint, procedure and work order. The required verification and approval must still be completed.
Q2. What if a torque record is associated with the wrong vehicle?
Keep the affected work package on hold and preserve the original data. Reconcile the tool event against the physical asset, maintenance order and approved records through the authorized process. Do not silently overwrite the original information.
Q3. Is a paint mark sufficient proof that a bolted connection has passed inspection?
No. A visual witness mark may be part of an approved inspection or maintenance procedure, but it does not independently establish the measured tightening result, asset identity or completion of the work package.
Q4. Why is shift handover important in bogie maintenance?
Because safety-related maintenance can involve several workers and shifts. Without a clear record of completed and outstanding operations, the next shift may not know which activities still require attention.
Q5. What should a railway maintenance team retain for fastener traceability?
Depending on the applicable specification, records may include part identification, material or batch information, tool records, operator details, inspection results, deviations, maintenance order references and authorized release documentation.
Conclusion: A Tool Pass Must Be Connected to a Complete Maintenance Record
Rail bolting maintenance records should do more than show that a tightening tool produced a successful result.
They should establish which vehicle was maintained, which joint was worked on, which procedure applied, which equipment and personnel were involved, and whether all required work was completed and authorized.
The Ottawa LRT case demonstrates why checklists, maintenance records, shift handover and qualified quality review must work together.
For railway maintenance teams, the objective is not simply to collect more digital data. It is to ensure that every important record belongs to the correct asset, the correct connection and the correct maintenance task.
Looking for industrial fasteners for railway-related applications?
Explore Flybear’s rail fastener application range and fastener quality inspection information.
For a product enquiry, provide the applicable drawing, connection location, standard, material or grade, dimensions, finish, quantity and required inspection documents.
Contact Flybear. Drawings, BOMs and specification attachments can be sent directly to biz@chinaflybear.com.
A supplier quotation or inspection report does not replace the railway operator’s maintenance approval, vehicle-specific procedure or required safety release.
Follow Me!


Need Fasteners for Your Application?
Share your application, standard or drawing, material or grade, dimensions, finish and quantity. Our team will review your requirements and recommend a suitable solution.