Metric Bolt Property Classes 8.8 vs 10.9 vs 12.9: How to Choose
8.8 vs 10.9 vs 12.9 bolts differ primarily in their specified mechanical property levels, but choosing the highest number is not automatically the safest engineering decision. Higher property classes can support greater bolt tension and potentially higher clamp loads for a given diameter, while also placing greater demands on the nut, female threads, coating process, installation control, and surrounding joint components. Industrial buyers should select the property class from the actual joint design rather than treating 12.9 as a universal upgrade from 8.8 or 10.9.
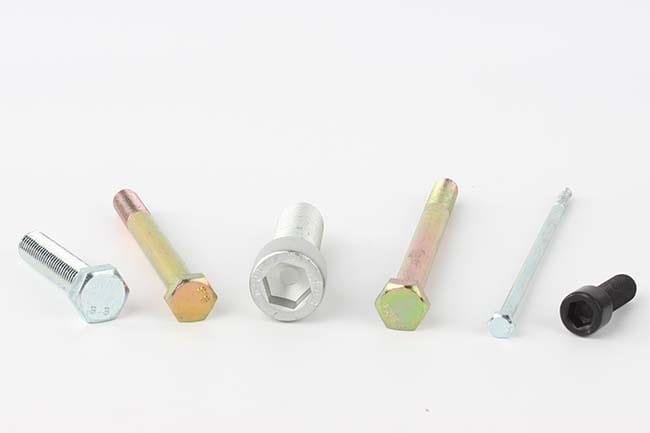
ISO 898-1 defines mechanical and physical requirements for applicable carbon-steel and alloy-steel bolts, screws, and studs with ISO metric threads. The property-class marking communicates important strength information, but it does not define corrosion resistance, fatigue life, tightening torque, coating performance, or suitability at every operating temperature. Those requirements must be specified separately.
8.8 vs 10.9 vs 12.9 Bolts: Quick Comparison
| Property Class | Nominal Tensile Strength Used in Designation | Nominal Yield Ratio | Nominal Yield Strength Used in Designation | General Selection Direction |
|---|---|---|---|---|
| 8.8 | 800 MPa | 0.8 | 640 MPa | Widely used high-strength class for machinery and general industrial joints |
| 10.9 | 1000 MPa | 0.9 | 900 MPa | Higher-load machinery, automotive, rail, and compact joints where additional bolt strength is required |
| 12.9 | 1200 MPa | 0.9 | 1080 MPa | Very high-strength applications where the complete joint, coating, installation, and mating components are designed accordingly |
These figures explain the property-class designation system; they should not be used as a substitute for the actual minimum mechanical requirements in the applicable ISO 898-1 tables. Minimum tensile, yield or proof-related requirements can depend on property class, diameter, product geometry, and the applicable test method. Always verify the current standard for order acceptance.
How Metric Bolt Property Classes Work
The two numbers in a metric property class communicate nominal strength information. For a class 8.8 bolt, the first number multiplied by 100 gives a nominal tensile strength of 800 MPa. The second number represents ten times the nominal ratio between yield-related strength and nominal tensile strength. A second digit of 8 therefore represents a ratio of 0.8, giving 800 × 0.8 = 640 MPa nominal yield strength.
The same logic gives 1000 MPa and 900 MPa for class 10.9, and 1200 MPa and 1080 MPa for class 12.9.
This designation is useful for understanding the relative strength level, but buyers should distinguish nominal designation values from the actual minimum acceptance values required by ISO 898-1. This distinction becomes important when checking certificates, tensile-test results, proof loading, hardness, and diameter-dependent requirements.
Class 8.8 Bolts: A Practical High-Strength Starting Point
Class 8.8 bolts are widely used in industrial machinery, equipment frames, brackets, mechanical assemblies, and other loaded joints where ordinary low-strength fasteners are insufficient. Their strength level makes them a practical starting point for many engineered carbon- and alloy-steel fastening systems.
Choosing 8.8 does not mean the application is lightly loaded. A correctly sized class 8.8 bolt can provide substantial clamping capacity. Increasing the property class should therefore follow a joint calculation rather than the assumption that a 10.9 or 12.9 bolt automatically creates a better connection.
Class 8.8 can be attractive where adequate strength, reasonable ductility, established manufacturing routes, and a broad range of coating options need to be balanced. The actual steel composition and heat-treatment route must still comply with the governing specification.
Buyers can review Flybear’s carbon and alloy steel bolt range when sourcing metric hex bolts, flange bolts, and drawing-based high-strength products.
Class 10.9 Bolts: Higher Strength for More Demanding Joints
Class 10.9 bolts provide a higher specified mechanical property level than 8.8 and are commonly considered where the joint requires greater bolt tension or where packaging limits make increasing the fastener diameter difficult.
Applications can include automotive powertrain and chassis assemblies, industrial machinery, rail equipment, heavy mechanical systems, and other engineered connections. Flybear’s automotive fastener solutions include applications where high-strength bolts are evaluated together with vibration, coating, torque, and dimensional requirements.
Moving from 8.8 to 10.9 does not simply increase the allowable tightening torque by a fixed percentage. The final tightening specification depends on thread size, pitch, friction, coating, lubrication, joint stiffness, target preload, and installation method.
The female thread also becomes important. If a high-strength 10.9 bolt is installed into a softer nut, aluminum housing, cast component, or insufficiently engaged tapped hole, the internally threaded component may become the controlling failure point before the bolt reaches its intended capacity.
Class 12.9 Fasteners: Maximum Strength Requires Greater Process Control
Class 12.9 fasteners occupy a very high strength level within the common ISO metric property-class system. They are frequently associated with high-strength socket screws and compact mechanical joints where substantial load capacity is required from a limited fastener size.
However, selecting 12.9 introduces additional design and procurement considerations. Higher strength does not eliminate joint separation, thread stripping, fatigue, embedment, coating failure, or installation variation. The surrounding components must be capable of using the additional bolt strength.
A class 12.9 bolt can be unnecessary if an 8.8 or 10.9 fastener already provides the required preload with suitable design margin. Over-specification may also narrow material, manufacturing, coating, and process-control options without providing a measurable improvement in the assembled joint.
Higher Strength Does Not Automatically Mean Better Fatigue Performance
Fatigue performance depends on the complete bolted joint rather than the property-class number alone. Important variables include preload, fluctuating external load, joint stiffness, thread geometry, thread runout, surface condition, manufacturing defects, stress concentration, and loss of clamp load.
A properly preloaded joint can reduce the alternating load experienced by the bolt, while an inadequately clamped connection can expose even a very high-strength fastener to damaging cyclic stresses.
ISO 898-1 defines specified mechanical and physical properties, but it does not itself provide a universal fatigue-life rating for each property class. Buyers should therefore avoid claims such as “12.9 lasts longer under vibration” unless the statement is supported by the actual joint design and validation testing.
For railway and rolling-stock applications where dynamic loading can be important, see Flybear’s rail fastener solutions.
Match the Nut and Female Thread to the Bolt
A high-strength bolt should never be evaluated independently of the internal thread. ISO 898-2 specifies mechanical and physical properties for applicable carbon- and alloy-steel nuts with defined property classes.
The correct nut class, nut style, thread engagement, and dimensions should be selected according to ISO 898-2, the relevant product standard, and the engineering requirements of the connection. Do not assume that any nut with the correct metric diameter is suitable for a 10.9 or 12.9 bolt.
For tapped holes, designers should check the female material, thread engagement length, wall thickness, and risk of thread stripping. This becomes particularly important when high-strength steel bolts are threaded directly into aluminum, cast iron, or another lower-strength material.
Coating Selection Becomes More Critical as Strength Increases
Carbon- and alloy-steel bolts often require a coating or surface treatment for corrosion protection, friction control, appearance, or assembly performance. Typical project specifications may call for electroplated systems, zinc-flake coatings, hot-dip galvanizing where applicable, phosphate systems, black oxide, or other engineered finishes.
The property class must be considered when choosing the coating process. High-strength steel fasteners can be sensitive to hydrogen embrittlement associated with certain manufacturing and surface-treatment processes. ISO 4042 includes requirements and recommendations intended to minimize hydrogen-embrittlement risk for electroplated steel fasteners.
This does not mean one coating should automatically be prohibited or required for every 10.9 or 12.9 bolt. The base material, hardness, cleaning process, coating system, post-treatment, dimensions, thread allowance, and project requirements must be reviewed as one controlled process.
Buyers should specify the actual coating standard and system instead of writing only “zinc coated” or “corrosion resistant.”
Torque Values Cannot Be Selected from Property Class Alone
A higher property class can permit a higher target preload when the complete joint is designed for it, but property class alone does not determine tightening torque.
Torque depends strongly on friction in the threads and under the rotating bolt head or nut. Zinc plating, zinc-flake coatings, sealers, topcoats, oils, waxes, and other lubricants can produce different torque-preload relationships even when bolt diameter and property class remain unchanged.
ISO 16047 provides standardized conditions for torque/clamp-force testing of applicable threaded fasteners and related parts. For controlled OEM applications, torque-tension testing of the actual fastener, nut, washer, coating, and lubricant combination can provide more useful assembly data than copying a generic torque chart.
Changing from 8.8 to 10.9 or 12.9 should therefore trigger a review of the installation specification rather than an automatic multiplication of the old torque value.
Temperature and Environment Can Change the Selection
ISO 898-1 mechanical properties are established under defined ambient-temperature testing conditions. Fasteners may not retain the same specified properties when exposed to substantially elevated or lower temperatures.
If the application involves an engine, exhaust system, furnace, cryogenic equipment, or another thermally demanding environment, buyers should provide the operating and design temperatures. Material composition, heat-treatment condition, exposure duration, preload, thermal expansion, and the clamped materials can all affect suitability.
Corrosion must also be treated separately from strength. A class 12.9 bolt has a higher mechanical property class than an 8.8 bolt, but the property-class number does not indicate corrosion resistance. The appropriate coating or alternative material system must be selected for the actual environment.
8.8 vs 10.9 vs 12.9 for Typical Industrial Decisions
| Engineering Situation | Selection Direction | What Must Be Verified |
|---|---|---|
| General loaded machinery joint | 8.8 may be a practical starting point | Joint load, preload, diameter, nut, fatigue, finish, and safety requirements |
| Higher-load compact machinery or automotive joint | 10.9 may be considered | Female-thread capacity, torque-tension behavior, coating process, fatigue, and component strength |
| Very high-load compact connection | 12.9 may be considered where specifically justified | Complete joint design, thread capacity, coating and embrittlement control, preload procedure, and inspection |
| Corrosive outdoor application | Do not select by property class alone | Coating system, corrosion environment, friction requirement, maintenance, and possible alternative materials |
| Elevated-temperature application | Verify temperature-specific suitability | Material, exposure duration, retained properties, preload, joint expansion, and governing specification |
Do Not Treat Metric Property Classes as SAE or ASTM Equivalents
Metric property classes and SAE or ASTM fastener grades use different specification systems. An approximate strength comparison may be useful during preliminary engineering, but it should not become a purchasing substitution.
For example, a buyer should not replace an ISO class 10.9 bolt with an SAE Grade 8 bolt simply because published tensile-strength levels appear similar. Thread system, dimensions, material requirements, proof properties, marking, test methods, coatings, and governing standards differ.
Flybear’s broader guide on how to choose bolt strength grade and material grade explains the distinction between metric property classes, SAE grades, and stainless-steel grade systems. The present guide focuses specifically on selecting between ISO metric classes 8.8, 10.9, and 12.9.
Inspection Requirements for High-Strength Metric Bolts
Inspection should be based on the ordered standard, property class, size, manufacturing route, surface treatment, and project requirements. Depending on the order, relevant checks may include material verification, hardness testing, tensile or proof-related testing, dimensional inspection, thread gauging, coating-thickness measurement, metallographic examination, and torque testing.
For high-strength fasteners, manufacturing control is especially important because final performance depends on both material and processing. Flybear supports carbon- and alloy-steel bolts using cold heading, hot forging, CNC machining, thread rolling, heat-treatment coordination, and surface treatment where applicable to the product and specification.
Buyers can review Flybear’s fastener quality inspection capabilities when defining the required acceptance and documentation scope.
Common Mistakes When Choosing Metric Bolt Property Classes
- Choosing 12.9 because it is the highest number: the joint may not require or benefit from the additional bolt strength.
- Using nominal designation values as certificate acceptance values: verify the actual ISO 898-1 requirements for the property class and size.
- Ignoring the nut or tapped hole: female-thread stripping can become the controlling failure mode.
- Assuming higher class means better fatigue life: fatigue depends on preload, joint stiffness, geometry, surface condition, and cyclic loading.
- Copying torque values between classes: torque also depends on coating, lubrication, thread geometry, and target preload.
- Ignoring hydrogen-embrittlement risk during coating: high-strength fasteners require controlled surface-treatment processes.
- Using property class as a corrosion rating: 8.8, 10.9, and 12.9 describe mechanical properties, not environmental durability.
- Equating ISO property classes with SAE or ASTM grades: cross-standard substitution requires engineering verification.
What to Include in an 8.8, 10.9 or 12.9 Bolt RFQ
For an accurate quotation and technical review, provide:
- Applicable ISO, DIN, EN, customer, or other product standard
- Required property class: 8.8, 10.9, or 12.9
- Bolt type, such as hex bolt, flange bolt, socket screw, stud, or custom component
- Nominal diameter, thread pitch, tolerance, length, and thread length
- Nut specification and property class, or tapped-hole material and engagement length
- Joint load, target preload, or assembly requirement where defined
- Coating, surface treatment, lubricant, and friction requirement
- Operating temperature and corrosion environment
- Dynamic, vibration, or fatigue-related application information where relevant
- Quantity and controlled drawing revision
- Required material, mechanical, dimensional, coating, and documentation inspection
FAQ: 8.8 vs 10.9 vs 12.9 Bolts
Is a 10.9 bolt always better than an 8.8 bolt?
No. Class 10.9 provides a higher specified mechanical property level, but 8.8 may already meet the required joint load. The correct choice depends on preload, diameter, female-thread strength, fatigue conditions, coating, environment, and the governing design specification.
Is a 12.9 bolt stronger than a 10.9 bolt?
Yes, property class 12.9 represents a higher nominal tensile and yield-related strength level than 10.9. However, the complete joint must be capable of using that additional strength, and manufacturing, coating, and installation controls may become more demanding.
Can I use the same nut when upgrading from 8.8 to 10.9?
Do not assume so. Verify the nut property class, style, dimensions, thread, and proof-load requirements against ISO 898-2 and the project specification. For tapped holes, verify the female material and required thread engagement separately.
Can I use the same torque when changing from 8.8 to 12.9?
No generic rule supports that substitution. The required torque depends on target preload, bolt size, thread pitch, coating, lubrication, bearing surface, and joint design. Establish the tightening procedure for the actual assembly.
Send the Joint Requirements Before Choosing the Highest Class
When requesting 8.8, 10.9, or 12.9 metric bolts, send Flybear the product standard or drawing, property class, diameter and thread, joint load or preload requirement, nut or tapped-hole information, coating and lubrication system, operating temperature and environment, quantity, and required inspection documentation. Use the Flybear contact page to submit your RFQ. Defining the complete joint allows the property class to be reviewed against actual mechanical and assembly requirements instead of selecting the highest-strength bolt by default.
Follow Me!